If you’ve spent any time in industrial fluid processing—whether in chemical manufacturing, food and beverage production, pharmaceutical filtration, or power generation—you already know sintered metal powder filters are workhorses. These porous media, made by fusing tiny metal particles (stainless steel, Hastelloy, Inconel, titanium, or even bronze) into a rigid, consistent structure, stand up to extreme temperatures, corrosive chemicals, and high-pressure conditions that would destroy disposable filter cartridges or even woven metal alternatives. But here’s the part that most plant operators and even some engineers don’t fully grasp: a sintered filter is only as useful as its ability to get back to peak performance after use. That’s where regeneration comes in, and the method you choose can make the difference between a filter that lasts years and one that needs replacement every few months, costing you thousands in downtime and materials. Sintered Metal Powder Filter
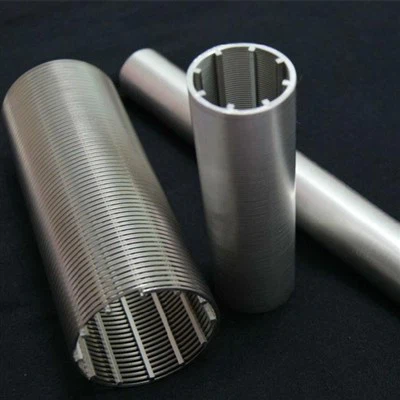
I’ve spent 12 years working alongside plant managers, maintenance crews, and process engineers as a sintered metal powder filter supplier, and I’ve seen first-hand how a small choice in regeneration can derail an otherwise robust filtration system. Let’s break this down: how different regeneration methods impact filter performance, what that looks like in real-world operations, and what you need to know to get the most out of your filter investment.
First, let’s set a baseline: what does “performance” even mean for a sintered metal powder filter? It’s not just about how much dirt it catches. It’s three interconnected metrics: 1) permeability (how easily fluid flows through the filter, directly affecting production rates), 2) retention efficiency (how well it captures the particles you’re targeting, from 0.1 micron to 100 microns, so your final product meets purity standards), and 3) mechanical strength (whether the porous structure stays intact under pressure or temperature cycles, avoiding costly filter failures and product contamination). When a filter is new, these metrics are consistent: for example, a 5-micron stainless steel filter might have a permeability of 100 L/min per cm², a retention rate of 99.9% for particles larger than 5 microns, and a tensile strength of 12,000 psi. After regeneration, if those metrics drop even 10%, you’re looking at slower production, potential product quality issues, or even a filter that can’t handle its operating pressure anymore.
Regeneration is essentially the process of removing the cake or gel that builds up on the filter’s surface and the particles trapped inside its pores. For sintered metal filters, this buildup isn’t just dust: it can be organic residues (from food processing, like sugar or yeast), inorganic scale (from water treatment, like calcium carbonate), catalyst fines (from pharmaceutical reactions), or even molten wax from petrochemical processing. The wrong regeneration method will either leave too much of this residue behind, or it will damage the porous structure itself.
Let’s start with the most common regeneration method: backwashing. This is exactly what it sounds like: you push a clean fluid (usually the same process fluid, or water, air, or nitrogen) in the reverse direction of normal flow to dislodge the trapped debris. For many low-to-moderate fouling applications, backwashing is cheap, fast, and easy to integrate into existing process systems. But how does it affect performance over time?
I worked with a craft brewery last year that was using 10-micron bronze sintered filters to separate yeast from beer. Initially, they were backwashing with cold beer every 4 hours, and their filters were lasting 6 months with only minor drops in permeability. But when they switched to a faster backwash cycle—every 90 minutes, to avoid shutting down production for filter change-outs—they saw a 25% drop in permeability after just 2 months. When we tested the filters, we found two issues: first, the high-velocity backwash was eroding the surface of the sintered metal. Tiny particle grains that held the porous structure together were breaking loose, widening the pores from 10 microns to over 15. That meant their retention rate dropped to 92%—enough that some yeast particles were passing through into the final beer, causing secondary fermentation in packaging. Second, the frequent backwashing didn’t give the yeast cake time to fully compact; instead, it pushed some yeast into the deepest pores, where it became trapped and couldn’t be dislodged even with backwash.
Another twist with backwashing: fluid choice matters. A lot of operators use compressed air for backwashing to cut costs, but if the air has moisture or oil in it, that can leave a residue on the filter surface that attracts more fouling over time. I had a customer in a chemical plant use compressed air for backwashing their 3-micron stainless steel filters used to purify caustic soda. After 10 regeneration cycles, the filter’s surface was coated with a thin layer of oil from the compressed air system, reducing permeability by 40% and making it impossible to get the filter clean again. They switched to nitrogen backwashing, which is dry and inert, and their filter performance went back to nearly new levels after each cycle, doubling the filter’s lifespan.
Next, let’s talk about another popular method for more stubborn fouling: ultrasonic cleaning. This uses high-frequency sound waves to create tiny bubbles in a cleaning fluid, which implode and dislodge debris from the filter pores. It’s great for delicate or narrow pore structures, and it can get into crevices that backwashing can’t reach. But here’s the catch: ultrasonic intensity has to be perfectly calibrated. Too high, and the sound waves will vibrate the sintered metal particles loose, breaking down the filter’s structure. Too low, and it doesn’t clean the pores effectively.
I had a pharmaceutical client who was using ultrasonic cleaning for their titanium sintered filters, which are used to remove catalyst fines from antibiotic solutions. Initially, they set the ultrasonic frequency to 40 kHz, which worked well—cleaning efficiency was 98%, and the filters retained 99.9% of their retention rate after each cycle. But when they tried to increase the frequency to 80 kHz to cut cleaning time in half, we saw three filters crack after just 5 regeneration cycles. The high-frequency vibrations created fatigue in the sintered metal bonds, especially in the thinner sections of the filter elements, leading to structural failure. They adjusted the frequency back to 40 kHz, and not only did the filters stop cracking, their lifespan extended from 12 cycles to 30. That’s a huge difference in cost—saving them over $15,000 a year in filter replacements.
Then there’s chemical cleaning, which is used for heavy fouling that neither backwashing nor ultrasonic cleaning can remove. This involves soaking the filter in a chemical solution—acid for inorganic scale, caustic for organic residues, oxidizing agents for stubborn oils—to dissolve the trapped debris. Chemical cleaning is highly effective, but it’s also the method that has the biggest impact on long-term filter performance if not done right.
I once worked with a power plant that was using sintered Inconel filters to purify boiler feed water. The filters were fouled with hard calcium carbonate scale, and they tried backwashing and ultrasonic cleaning with no success, so they switched to a 20% hydrochloric acid (HCl) solution for chemical cleaning. After just two cycles, the filters’ permeability dropped by 35% and they developed small holes in their structure. Why? HCl is highly corrosive to Inconel if the pH isn’t carefully controlled. The plant didn’t neutralize the acid after each cleaning cycle, so residual acid slowly etched away the sintered metal particles, widening the pores and weakening the structure. When we recommended they use a 5% HCl solution with a neutralization step (rinsing with water and a mild base after cleaning), their permeability recovered to 90% of its original level after each cycle, and the filters didn’t develop any structural issues.
Another point about chemical cleaning: compatibility with the filter material. For example, if you use a strong oxidizing agent like hydrogen peroxide on a bronze filter, it will react with the copper in the metal, causing pitting that can damage the filter over time. Always check the filter material’s chemical resistance before choosing a cleaning solution—something as simple as checking a material compatibility chart can save you thousands in replacement costs.
What about regeneration for specific application types? It’s not one-size-fits-all. For example, in food and beverage applications, you can’t use harsh chemicals, so backwashing with process fluid or ultrasonic cleaning with food-grade water is the way to go. In petrochemical applications, where fouling can be heavy and include hydrocarbons, a combination of backwashing with nitrogen followed by a mild chemical cleaning is often the best approach. In aerospace, where filters are used for fuel purification and have to withstand extreme conditions, ultrasonic cleaning is preferred to avoid contamination from chemicals that could affect fuel performance.
I want to emphasize that there’s no “best” regeneration method in isolation. It depends on your filter material, pore size, the type of fouling, your operating conditions, and your budget. But the key takeaway is that every regeneration step impacts performance, and even small missteps can lead to big problems down the line.
Over the years, I’ve developed a simple framework for customers to follow when choosing a regeneration method. First, test a small sample of your filter with different regeneration methods to see how performance holds up after multiple cycles. Second, track metrics like permeability and retention rate after each cycle—if you see a steady drop, that’s a sign your regeneration method is damaging the filter or not cleaning it enough. Third, work with a supplier who understands both sintered metal filter design and industrial processing, not just selling products. Too many operators buy a filter and then figure out regeneration on their own, which can lead to unnecessary failures.
If you’re in the market for sintered metal powder filters, or you’re struggling with poor filter performance due to bad regeneration, I can help. We’ve worked with hundreds of companies across industries to customize filter designs and regeneration protocols that extend filter lifespan, improve production rates, and reduce product contamination costs. Whether you’re looking to test a new filter, adjust your existing regeneration process, or troubleshoot recurring filter issues, we can provide tailored solutions for your specific needs.

To discuss your filtration and regeneration requirements, feel free to connect with our team to arrange a procurement consultation. We’re ready to help you find the right solution to boost your process efficiency and lower operational costs.
Wedge Wire Filter Screen References:
- Tadeusz, J., & Andrzej, Z. (2018). Regeneration of sintered metal filters: Impact of method on pore structure and performance. Journal of Porous Materials, 25(3), 897-908.
- Smith, A. B., & Lee, M. S. (2020). Industrial filtration: A guide to sintered metal filter maintenance and regeneration. Industrial Press, Inc.
- Garcia, R., et al. (2021). Ultrasonic cleaning parameters for sintered metal filters: Calibration for optimal performance. Separation and Purification Technology, 266, 118542.
- Patel, N. K., & O’Connor, L. (2019). Chemical regeneration of sintered metal filters: Compatibility considerations for process fluids. Chemical Engineering Journal, 365, 447-456.
- International Organization for Standardization. (2017). ISO 13465:2017 – Filtration performance testing of porous metal materials. ISO, Geneva.
Henan Easy Filter Equipment Co., Ltd.
As one of the leading sintered metal powder filter manufacturers and suppliers in China, we offer a wide range of products with superior quality. Please rest assured to buy advanced sintered metal powder filter from our factory. We also accept customized orders.
Address: Apartment No.1, Building No.2, Zhengshang Jinyushijia, Xinzhong Street, Xinxiang, Henan, China.
E-mail: vivian@easyfiltertech.com
WebSite: https://www.easyfilter-china.com/
